Hey there, let’s cut to the chase – if you’re reading this, chances are you’ve got ASME flanges in your operation and you’re sick of wasting time (and money) on preventable leaks, premature failures, or last-minute replacements that throw your whole project off. I’ve been in the ASME flange supply game for over 12 years now, and let’s be real – most folks treat these flanges like set-it-and-forget-it parts, only to panic when something goes wrong. That’s exactly why I’m breaking down the straight, no-BS guide to maintaining ASME flanges the right way – and as a supplier who’s seen every mistake in the book, I’m giving you the tips I actually pass to my clients, not the fluff you’ll find in outdated industry manuals. ASME Flange

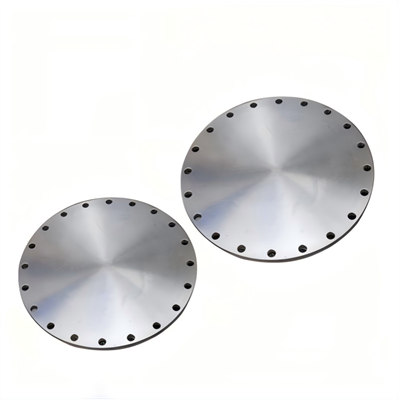
First, let’s get one thing straight: ASME flanges aren’t all the same. You’ve got your different classes (150, 300, 600, even 900 for heavy-duty stuff), types (weld-neck, slip-on, blind, threaded), and materials – carbon steel, stainless, alloy, even exotic stuff for high-temp or corrosive lines. The maintenance rules shift a little depending on what you’re working with, but the core principles stay consistent. I once had a client with a $50k refinery shutdown because they messed up a 300-class alloy steel blind flange – they’d used a generic torque number instead of checking the ASME B16.5 specs for that exact material, and it blew a leak after 3 days. Ouch. Don’t be that guy.
Let’s start with the first line of defense: pre-installation checks. So many failures start before the flange even touches the pipe. When you get flanges from a supplier (ahem, like mine), don’t just unbox ’em and slap ’em on. First, do a visual inspection for dings, scratches, or rust – especially on the sealing faces. Even a tiny 0.5mm scratch on a raised face flange is enough to cause a leak. I always tell clients to use a straightedge or a feeler gauge to check for warping too; if the flange face is more than 0.005mm out of flat, toss it.
Next, pipe prep. The pipe end needs to be cut perfectly square, no burrs, and aligned so it’s not stressed. If the pipe is even a little off-center when you weld on a weld-neck flange, that’s uneven pressure when you bolt it up, and the gasket won’t seat right. I see this all the time – someone rushes the fit-up, skips the pipe bevel for weld-neck flanges, and then wonders why the joint leaks after a pressure test. Take an extra 10 minutes to measure the pipe’s outside diameter, match it to the flange’s bore, and make sure the gap between the pipe and flange neck is consistent around the whole circumference.
Gaskets are another big one here. Most people grab whatever gasket’s lying around, but that’s a no-no. For ASME flanges, you need a gasket rated for your class, material, and service conditions. If you’re working with high temp (over 500°F), don’t use a soft rubber gasket – go with spiral-wound or graphite. For corrosive fluids, use PTFE or stainless steel jackets. Also, never reuse gaskets. Even if it looks brand new, compressing it once kills its elasticity, so you’ll get leaks when you retorque later. I once had a client try to save $5 on a gasket and end up paying $2k in downtime – that’s a trade that never makes sense.
Now, the part everybody messes up: bolt torqueing. This is where 90% of flange leaks come from. You can’t just tighten bolts in a circle (crisscross pattern, duh) and torque ’em to a random number. First, check the ASME B16.5 or your project specs for the exact torque value – it depends on bolt size, class, material, and even the flange size. For example, a 1-inch 304 stainless bolt on a 300-class flange has a totally different torque spec than a 2-inch carbon steel bolt on a 600-class.
But here’s the pro tip: don’t torque all bolts in one go. Do it in 3 to 5 sequential passes, each time cranking the torque up to about 50%, 75%, and 100% of the final value. That evens out the pressure across the flange face so the gasket seats uniformly. Also, use a calibrated torque wrench – and calibrate it every 6 months, minimum. I’ve seen guys use a wrench that’s off by 20 ft-lbs and wonder why half the bolts are too loose and half are snapped. If you’re working with high-pressure lines, use a bolt tensioner instead of a torque wrench – it’s way more accurate for big bolts.
Once the flange is installed, the real maintenance starts. It’s not “set it and forget it” – you need regular checks, especially in the first few weeks after installation, because gaskets can settle. I tell clients to do a walkaround every 7 to 10 days for the first month, then once a month after that. What to look for? Leaks (drips, seepage, even a shiny spot on the flange face that’s a fluid residue), rust buildup on bolts or flange faces, and any signs of vibration – if the pipe is vibrating a lot, that puts stress on the flange bolts and will loosen them over time.
Oh, and when you do those checks, take notes. Track torque values, check dates, and any issues you find. That way, if you have a failure, you can look back and see if it was a bad install, a wrong gasket, or normal wear. I had a client who caught a loose bolt on a 150-class flange during a routine check – if he’d waited another week, the leak would’ve caused a shutdown. Small checks = big savings.
Retorquing is a big part of maintenance too. Most ASME flanges need a retorque 24 to 48 hours after initial installation, and another one after a week or so, especially if you’re dealing with cyclic loads, high temps, or vibration. Why? Because the gasket compresses a little, and the bolts loosen from thermal expansion/contraction or pipe movement. Rule of thumb: if you see even a tiny seepage, retorque – don’t wait for a full leak. Just remember to follow the same crisscross, sequential pass method you used for initial torque, or you’ll mess up the gasket seat and cause more leaks.
Now, what about long-term storage? I know not everyone’s installing flanges right away, but storing them wrong ruins them before you even use them. If you have spare ASME flanges, keep them in a dry, covered area, off the ground (so they don’t sit in water or moisture). Wrap the sealing faces in plastic to prevent rust, and don’t stack heavy stuff on top of them – that warps the flange face. For flanges made of exotic materials (like titanium or Hastelloy), even more care – keep ’em away from carbon steel flanges during storage to prevent galvanic corrosion. That’s a mistake I see on construction sites all the time – guys toss a titanium flange on top of a carbon steel one, and by the time they use it, the sealing face is corroded.
Wait, let’s talk about common mistakes I see day in and day out, because these are the ones you need to avoid at all costs. First, using the wrong class flange for the job. A 150-class flange is fine for low-pressure gas lines, but if you put that on a high-pressure steam line (over 100 PSI), it’s going to fail. Always match the flange class to your system’s maximum pressure and temperature – ASME B16.5 has a pressure-temperature rating chart, so refer to that, not what looks right.
Second, ignoring corrosion. Even stainless steel flanges can corrode if they’re exposed to saltwater, chemicals, or acidic fluids. If you’re working in a corrosive environment, use flanges with a protective coating (like epoxy) or choose a higher-grade material. And do regular cleaning – use a soft brush and mild detergent to clean flange faces, not wire brushes, which scratch the sealing surface. Wire brushes on ASME flange faces are a cardinal sin in my book – I’ve seen a 6-inch stainless flange ruined by 5 minutes of wire brushing.
Third, mixing up bolt materials. If your flange is carbon steel, don’t use stainless steel bolts – that causes galvanic corrosion if they’re in contact with a fluid that conducts electricity (like water). Match the bolt material to the flange material, or use a compatible coating to prevent that. Same goes for stud bolts and nuts – don’t mix different grades, because they’ll seize up when you torque them. I once had a client that snapped two stud bolts because he used a Grade 2 nut on a Grade 8 bolt – they seized together, and when he tried to loosen it, the bolt broke.
Let’s get practical with an example. Suppose you’re installing a 6-inch 300-class weld-neck carbon steel flange on a water line at 150 PSI. Here’s the step-by-step maintenance flow:
- Unbox the flange, check sealing face for scratches/warping with a straightedge.
- Prep the pipe: cut square, remove burrs, align to the flange, tack weld it in place.
- Pick a full-face EPDM gasket (rated for water, 300 PSI).
- Torque bolts in crisscross passes: 50 ft-lbs, 75 ft-lbs, 120 ft-lbs (that’s the spec for 1-inch Grade 8 bolts on this flange) over 10 minutes total.
- Do a pressure test to check for leaks.
- Retorque after 24 hours, then again after 7 days.
- Do a visual check every 10 days for the first month, then monthly.
Simple, right? But if you skip even one step, you risk a leak.
Now, what about when things go wrong? If you spot a leak, don’t panic – but don’t ignore it either. First, shut down the line if it’s safe, then figure out the cause. If it’s a small seepage, maybe it just needs a retorque. If it’s a big leak, you might need to replace the gasket or even the flange. And if a bolt is snapped or corroded, don’t just grab any old bolt – use the exact material and grade the specs call for. Using a wrong bolt here will lead to another failure fast.
Let’s talk about why I know this stuff works. I’ve supplied ASME flanges to refineries, power plants, food processing facilities, and even offshore drilling rigs over the years. The clients that stick with me are the ones that follow these basics – the ones that cut corners end up calling me at 2 a.m. begging for a replacement flange because their line blew. Look, I’m here to sell flanges, but I’m also here to make sure my clients’ projects don’t go sideways because of bad maintenance. That’s why I give these tips for free – it’s not just good for them, it’s good for our relationship long-term.
Before I wrap this up, let’s hit one last point: if you’re ever unsure about your flange specs, maintenance steps, or need high-quality ASME flanges that meet all the ASME B16.5 standards, don’t guess. Reach out to get in touch to discuss your needs. We don’t cut corners on our flanges – every single one we supply goes through a pre-shipment check to make sure the sealing face is flat, the material is correct, and the specs match what you ordered. And if you have questions about maintenance, our team can walk you through whatever you need – from torque specs to gasket selection.
At the end of the day, maintaining ASME flanges isn’t rocket science. It’s about paying attention to the details: pre-install checks, right gaskets, proper torque, regular inspections, and using the right parts. Skip the shortcuts, and you’ll save yourself so much headache (and money) down the line. I’ve seen too many businesses lose big because they overlooked simple flange maintenance – don’t let that be you.
Pipe Fittings References:
ASME B16.5, Pipe Flanges and Flanged Fittings, 2020 Edition
API 6A, Specification for Wellhead and Christmas Tree Equipment, 22nd Edition
NACE SP0177, Standard Practice for Corrosion Control of Steel Equipment in Sour Gas and Oil Environments, 2021 Edition
Hebei Haihao Group Huadian High Pressure Pipe Fittings Co., Ltd.
As one of the most professional asme flange manufacturers and suppliers in China, we are able to meet the needs of the majority of our customers. Please rest assured to wholesale high quality asme flange made in China here from our factory. For price consultation, contact us.
Address: Donglin Industrial Zone, Mengcun County, Cangzhou City, Hebei Province, China
E-mail: haihaohuadian@outlook.com
WebSite: https://www.hhfittings.com/
