If you’ve ever worked with CNC turning, or reached out to a CNC turning supplier for a custom part quote, you’ve probably seen “spindle speed” listed on our tech specs, maybe next to a note that it’s one of the most impactful variables in the entire machining process. When I first started in this industry—back when most of our jobs were manual lathe work and we only upgraded to CNC machines in the early 2000s—I had a rough idea it meant how fast the part spins, but I had no clue how much it could make or break a part. Over 20 years of running CNC turning projects, troubleshooting every miscut and tool wear disaster you can imagine, I’ve come to see spindle speed as less of a number on a sheet and more of a core pillar that ties together material selection, tooling, and end part quality. Let’s break this down the way I explain it to new engineers and small business owners who come to us confused about their part requirements. CNC Turning
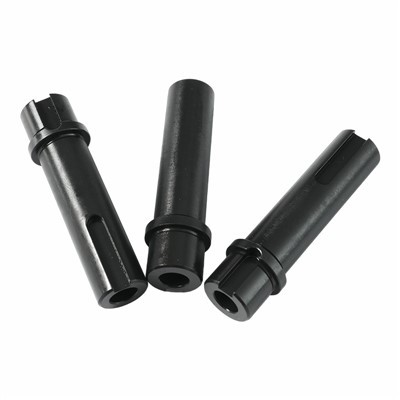
First, let’s get the basic definition out of the way, because it’s simpler than it sounds: spindle speed (almost always written as SFM or RPM in our shop) is the rotational speed of the part mounted in the CNC lathe’s chuck, measured in revolutions per minute (RPM). The cutting tool stays stationary as the part spins, so the “surface speed” of the part’s outer diameter is what actually interacts with the tool edge. Wait, I said SFM—surface feet per minute—so why do we mix RPM and SFM? That’s the first thing most people get wrong, and it’s the reason so many new machinists end up with broken tools or rough parts. SFM is the actual speed of the material’s surface as it passes the cutting tool, a standard that’s universal across the industry, while RPM is the speed the lathe’s spindle runs at, which changes depending on the part’s diameter. You can calculate RPM from SFM with a basic formula: RPM = (SFM × 12) / (π × diameter of part, in inches). Let me give you an example to make this real—last month we were turning a 6-inch diameter aluminum valve body for a farm equipment manufacturer. We needed a surface speed of 1,200 SFM for the carbide inserts we use (more on that in a minute), so plugging into that formula, our spindle speed came out to around 764 RPM. If that same part had been only 2 inches in diameter, to hit the same 1,200 SFM we’d crank the spindle up to 2,292 RPM. That’s a critical distinction, especially for smaller parts that need to spin fast to get optimal surface speed.
Now, why does this number matter so much? For us as a CNC turning supplier, it’s not just a technical detail—it’s the difference between a part that passes inspection on the first run and a job that requires three re-makes, wasted material, and missed deadlines. The first big factor is tool life. Every cutting tool—whether it’s a carbide insert, a high-speed steel bit, or a diamond tool—has a recommended SFM range for the material it’s cutting. If you run too slow, the tool rubs against the part instead of cutting, creating friction that builds up heat, dulls the edge fast, and leaves a rough surface finish. Run too fast, and the tool edge overheats, chips, or even breaks mid-cut, which can scratch the part or jam the lathe. Last year we had a customer bring in a batch of 1-inch diameter brass bushings they’d had machined locally; the shop there had run them at half the correct SFM, so the tooling wore out after 10 parts, costing them way more than if they’d just adjusted their spindle speed. We re-ran the same batch at the right SFM, and each tool cut 50 parts without a single flaw.
Next up is material type. That’s the biggest driver of spindle speed, hands down. Soft, non-ferrous materials like aluminum, brass, and plastic can handle much higher SFM, which means higher RPM for their diameter, because they cut easily and don’t generate as much heat. Our go-to SFM for 6061 aluminum, the most common grade we work with, is between 800 and 1,500 SFM. We’ll push closer to 1,500 SFM for smooth, light cuts, and drop to 800 for heavier roughing passes that remove more material fast. For harder ferrous materials like stainless steel or tool steel, we have to slow way down. 304 stainless, for example, only handles around 200 to 500 SFM, because it’s tougher, generates more heat, and can work-harden if cut too fast—meaning the outer layer of the part gets harder as the tool cuts, making it even more difficult to machine. Tool steel can be even lower, sometimes as low as 100 SFM, if we’re working with heat-treated grades. Then there’s exotic materials, like titanium or Inconel, which we see more of for aerospace and medical parts. Titanium is tricky—it’s strong, generates a lot of heat at the cutting edge, so we run at 100 to 300 SFM, and we use tools with special heat-resistant coatings to avoid melting or chipping. Inconel is even slower, usually 50 to 200 SFM, because it’s designed to withstand high temperatures, so cutting it wears out tools super fast if speed isn’t dialed in right.
I should also mention roughing vs finishing passes, because that’s another place spindle speed changes. Roughing is the first step when we’re cutting a lot of material off the part, so we usually run at a slightly lower SFM (and higher feed rate) to remove as much material as quickly as possible without damaging the tool. Finishing is the final pass, where we’re only removing a few thousandths of an inch to get the part’s exact dimensions and a smooth surface finish. For finishing, we bump up the spindle speed a bit—higher SFM means the tool cuts more cleanly, leaving a smoother surface that rarely needs extra polishing. For that aluminum valve body I mentioned earlier, roughing runs at 800 SFM, and the finishing pass jumps up to 1,200 SFM, which gave us a Ra (surface roughness measurement) of 16 microinches on the outer diameter—well within the customer’s requirement of 20.
A lot of people, especially new clients who come to us with simple parts, think spindle speed is just something the CNC machine handles automatically, and while modern lathes do have built-in controls that adjust RPM automatically based on SFM, that only works if the machinist programs in the right SFM and takes the part diameter into account. That’s where our experience as a CNC turning supplier pays off—we don’t just plug numbers into a machine. We account for everything: the tool brand and coating, the machine’s rigidity (some older lathes can’t handle high RPM without vibration), the part’s size and shape, and even the finish the customer needs. For example, if a customer is making a small medical screw out of titanium, we’ll use a diamond-coated carbide tool, run at the correct SFM, and adjust the spindle speed for each tiny diameter segment of the screw’s thread to ensure consistent cuts that meet FDA tolerances.
I’ve seen too many shops cut corners on spindle speed, especially for small, low-batch jobs where they think it’s not a big deal. But last month we had a custom motorcycle part client who brought in a part that another shop had messed up: they’d run a 1.5-inch titanium part at double the correct SFM, so the tool chipped, left a scratch in the critical seal surface, and the part was rejected by the client’s quality team. We re-machined the part, took the time to set the spindle speed correctly, and it passed inspection on the first try. That’s the kind of difference getting spindle speed right makes—it’s not just a technical number, it’s part of delivering a part that works as intended.
Now, let’s talk about common mistakes we see people make when calculating spindle speed, because that’s probably why you’re here, if you’re a small business owner or engineer trying to get custom parts machined. The biggest one is mixing up SFM and RPM. Like I said earlier, RPM is useless on its own because it changes with part diameter. A lot of people will see a spindle speed of 3,000 RPM on a part and think that’s the same for every part, but if you have a 4-inch diameter steel part and a 1-inch diameter aluminum part, 3,000 RPM is way too fast for steel and way too slow for aluminum. Another mistake is not accounting for tool coating. A basic uncoated carbide tool has a lower SFM limit than a TiN or TiCN coated tool, because the coating reduces friction and heat. If you use the same SFM for an uncoated tool as you would for a coated one, you’ll get poor tool life. And don’t forget machine rigidity—if you’re running on an older, less stable lathe, high RPM can cause vibration, which leads to a rough surface finish, so you might have to lower SFM even if the material can handle higher speeds.
For anyone who’s not familiar with machining terms, you might be wondering why we don’t just use metric units everywhere, but SFM is still the standard in North America, especially for custom CNC turning work. If you work with a supplier in Europe or Asia, they’ll use SMM (surface meters per minute), but the formula is almost identical, just swapping inches for millimeters. When we get a quote request, we always ask for the material, part diameter, finish requirements, and type of passes (roughing vs finishing) first, because that’s what we need to dial in the correct spindle speed.
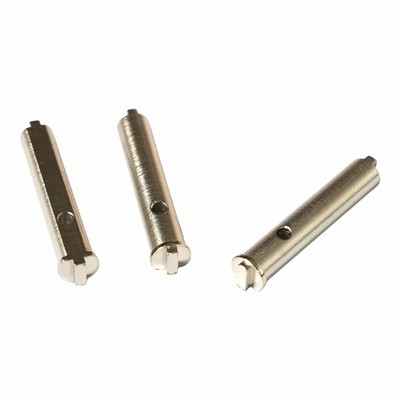
At the end of the day, spindle speed is just one variable in CNC turning, but it’s the foundation of every other decision we make as a CNC turning supplier. Get it right, and you get consistent tool life, minimal waste, parts that meet all your specifications, and on-time delivery. Get it wrong, and you’ll face delays, extra costs, and parts that don’t work for their intended use. If you’re working on a project and you’re not sure what spindle speed is right for your part, or you need a reliable CNC turning supplier that can help you work through those details, we’re here to walk you through every step. Whether you need a single prototype or a high-volume production run, we’ll take the time to get the spindle speed, tooling, and every other detail right so your parts come out exactly as you need them.
Stainless Steel Turned Parts Reference:
ASTM International. (2020). Standard Practice for Speed, Feed, and Tool Life in Machining. ASTM B211-20, Standard Specification for Aluminum and Aluminum-Alloy Bar, Rod, and Wire.
DeGarmo, E. P., Black, J. T., & Kohser, R. A. (2011). Materials and Processes in Manufacturing (11th ed.). John Wiley & Sons.
Society of Manufacturing Engineers. (2018). CNC Turning: Fundamentals and Applications. SME Press.
Huizhou Quanyi Precision Hardware Products Co., Ltd.
We’re well-known as one of the leading CNC turning manufacturers and suppliers in China, featured by quality products and good service. Please rest assured to buy customized CNC turning made in China here from our factory. Contact us for more details.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
