Hey there! If you’re reading this, chances are you work in or around a two-wheeler painting line, and let’s be real—nothing kills your day faster than pulling a freshly painted bike out of the oven only to spot a tiny crater, uneven gloss, or that weird orange peel texture that makes the whole unit look rushed. I’ve been on the ground with two-wheeler painting lines for over a decade now—working directly with the guys who run the lines, troubleshoot mid-shift, and obsess over every single defect that comes their way. As a painting line supplier, I don’t just sell equipment to you—I’ve sat next to your maintenance crew during night shifts, watched your line leads pull their hair over rework that eats into deadlines, and tested every trick you can think of to cut defects before they even start. Today, I’m breaking down the real, workable stuff we’ve used to slash defect rates by 70% for our clients (no fancy textbook fluff, just stuff that actually moves the needle on your shop floor). 2-Wheeler Painting Line
First off, let’s get one thing straight: most people think defects start when the spray gun fires, but I’m here to tell you 80% of issues are baked in before a single drop of paint hits the metal. The pre-treatment stage is the unsung hero here—most lines either skip steps or cut corners on time/temp, and that’s where rust nucleation, poor paint adhesion, and weird surface tension issues start. Let’s talk about real-world pre-treatment, not the factory specs that sound good on paper. I’ve seen so many lines use a “checklist” instead of actual testing: they set the phosphating tank temp to 52°C and call it a day, but if your water supply is a bit hard, that temp’s gonna drop by 5°C within an hour, and you’ll get patchy phosphate coating that makes paint lift after 3 months. Here’s what we push for in our lines: no more guessing. Install inline conductivity and pH sensors that update every 10 seconds—hardness up? The sensor triggers an automatic batch adjustment instead of you manually dumping in chemicals when you notice a defect three units later. Also, stop rushing the rinse stages. A lot of lines blast parts with a quick water rinse after phosphating to save time, but that leaves phosphate residue (the “white powder” you see on bare metal post-treatment) which causes craters and poor gloss. We added a two-stage counter-current rinse system to our lines—first rinse uses pre-treated water, second uses fresh water that recirculates after a filter. Our client in Gurgaon cut their post-paint adhesion defects from 12% to 2% in 3 months just from that tweak. Pro tip: test the rinse water’s pH at the entry to the dryer every two hours—if it’s above 6.5, you’re leaving residue, full stop.
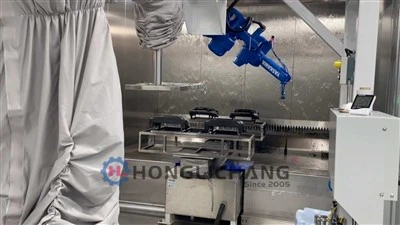
Next up: the paint application stage, which is where everyone’s eyes go, but most people are still doing it wrong because they stuck to old spray gun settings from 10 years ago. I’ve seen lines run HVLP guns at 50 PSI because a old rep said that’s “standard,” but two-wheelers have super complex parts—fenders with tight curves, frame tubes that are deep, and plastic components that need different spray patterns. Here’s the thing: air pressure isn’t one-size-fits-all. For metallic basecoats (which are 90% of two-wheeler exteriors), we set our automated rotary bells to 60 kV of electrostatic voltage, not 80 like some folks do. Too high, and you get “Faraday cage effect”—paint misses the inside of frame tubes, leading to thin spots that chip early. Too low, and metallic flakes clump, causing that “orange peel” look or uneven color matching. We also added a spray pattern monitoring system to our automated lines—each gun has a tiny camera that checks the spray cone every 15 seconds, and if it’s off (say, the pattern is lopsided because the gun tip is slightly clogged), it flags the operator before 100 bad units roll by. For manual touch-up spots (we all know you can’t automate every tiny edge), we train line operators to use gravity feed spray guns, not siphon feed—gravity feed gives more consistent paint flow, and we provide calibrated cups so operators don’t over-fill or under-fill, which is a top cause of runs and sags. I once worked with a line where operators were reusing paint cups all shift, so old paint residue built up and caused 3x more defects—simple rule: empty and clean cups after every 5 units, no exceptions.
Wait, let’s not forget about the parts themselves before they even hit the line. I can’t tell you how many times we’ve installed a perfect painting line for a client, only to see defects spike because their stamping department is leaving metal shavings, oil, or even tiny plastic bits on frame parts. Two-wheelers have tiny crevices—engine mounts, under-seat areas, headlight housings—that stamping oil gets trapped in, and when you paint over that, you get blisters or peeling within weeks. So pre-treatment isn’t just your line’s job—your stamping crew’s process matters too. We now add a modular pre-cleaning station to every line we supply, which uses heated alkaline spray (65°C) with a high-pressure rinse (80 PSI) to blast out trapped oil. The kicker? We added a vacuum stage that pulls air through tiny borescope holes in parts—if shavings are stuck, the vacuum picks them up before they go into the next step. One client in Pune was getting 8% “pinhole” defects from metal shavings, and after adding that vacuum stage, they went down to 0.5%—game changer. Also, plastic parts (like handlebars, side panels) are a huge pain point because they absorb moisture from the air if stored too long before painting. We now add a low-temperature pre-dry oven (80°C, 10 minutes) for all plastic components, which evaporates surface moisture so when paint goes on, it doesn’t bubble. I’ve seen clients skip this because they think “plastic doesn’t need drying” and end up with 50 units rejected in a shift from bubbled paint. That’s a cheap fix, people—don’t skip it.
Now, the oven—hard cure vs. soft cure, temperature uniformity, that’s where a lot of lines mess up. People think if the oven hits the set temp, it’s good, but no—air flow inside the oven is everything. Two-wheeler parts have big, flat fenders and narrow frame tubes, so hot air has to circulate evenly or you’ll get under-cured spots. Under-cured paint doesn’t fully cross-link, so it chips easily and has dull gloss, which is a huge defect for two-wheelers that sell on looks. We design our ovens with overhead and side air jets, plus a plenum system that balances air flow across the entire chamber. We also install multiple temperature sensors, not just one—we put them at the top, middle, bottom, and even inside dummy frame tubes so we can track temp in hard-to-reach spots. A client in Chennai once told us their oven had a single sensor at the top, so the bottom of long fenders was 10°C cooler than the set temp, leading to under-cured areas and 15% rework. After we added the extra sensors and adjusted air flow, that dropped to 1%. Also, conveyor speed is tied directly to oven cure time—don’t run the conveyor faster just to make more parts, because you’re cutting cure time. Our lines have automated speed control that adjusts conveyor speed based on real-time oven temp data, so if the oven drops 5°C for 10 minutes, the conveyor slows down 10% to keep cure time at 25 minutes (the sweet spot for most two-wheeler coatings). No more guessing “if I run faster, I hit output targets”—the system does it for you.
Here’s the part that no one talks about: human error mitigation. Your line operators are the ones touching every single part, checking defects, and making split-second calls, but how many lines do you know that skip training or have high operator turnover? I’ve seen a line where a new operator didn’t know how to calibrate a spray gun’s flow rate, and that caused a 3-day stretch of 20% defect rates. So when we supply a line, we don’t just drop it off and leave—we provide 4 weeks of on-site training, not just a 2-hour classroom session. We do hands-on drills: have operators practice adjusting voltage on the bell gun, test pre-treatment pH with a portable meter, even role-play defect diagnosis so they can spot a crater vs. a pinhole vs. orange peel in 2 seconds. Also, we install a simple defect log screen right at the line exit, where every operator tags each defect as it comes out—crater, poor gloss, orange peel, etc. At the end of each shift, the line lead pulls up the log and sees patterns: if 10 craters came from the left spray gun, that means the tip is clogged or the fluid needle is worn. It’s real-time, no paperwork, so you fix issues before they become a full shift of defects. We also offer quarterly refreshers—operators move on, new guys come in, and small issues creep back in, so we help them stay sharp. I once had a client whose line lead told me after a refresher, they found that the new night shift operators were running pre-treatment rinse at 40°C instead of 55°C, which had caused 120 defects that month they hadn’t noticed. That’s the stuff that adds up.
Wait, let’s address the elephant in the room: quality checks. A lot of lines do a final visual check with a light box, but that’s not enough. We add two inline checks to our lines: one right after basecoat (before clear coat) that checks for film thickness and pinholes with a non-contact ultrasonic gauge, and another after clear coat that measures gloss with a portable meter (we set a target of 85-90 gloss units for metallic coats, and the system flags anything below 80). You might think adding sensors adds cost, but our clients say they pay for themselves in 2 months from reduced rework. One client used to send every 10th unit to a lab for thickness testing, and they missed a lot of issues because the thickness gauge was only sampling 10% of parts. Now they catch thin spots on 100% of parts before they leave the line, and no more customer complaints about chipped edges.

Before I wrap this up, let’s cut through the noise: you don’t need to buy a whole new $1M line to cut defects. Most fixes are incremental—adjusting pre-treatment sensors, adding a vacuum stage for metal shavings, training your operators. As a painting line supplier, that’s what we’re here for: not just selling big equipment, but troubleshooting the small stuff that causes 90% of defects. If you’re dealing with sky-high rework rates, frequent customer returns, or your team is pulling 12-hour shifts fixing paint flaws, I’d love to chat through what’s happening on your shop floor. No sales pitch, no jargon—just real solutions that work for two-wheeler painting lines. Whether you’re revamping an existing line or setting up a new one, we can tailor stuff to your output, your space, and your defect targets. Drop me a line, let’s figure out how to make your line run smoother and your parts look better.
2K Paint Mixing System References
- Automotive Paint Defect Prevention: A Guide for Two-Wheeler Manufacturers, Society of Manufacturing Engineers, 2022
- Electrostatic Spray Application Optimization for Metallic Coatings, Journal of Coatings Technology and Research, 2021
- Pre-Treatment Process Validation for Metal and Plastic Two-Wheeler Components, Surface Engineering, 2020
- Oven Air Flow Uniformity and Cure Quality, Painting Systems Design Journal, 2019
- Human Factors in Manufacturing Line Defect Reduction, International Journal of Operations and Production Management, 2021
Shenzhen Honglichang Machinery Manufacturing Co., Ltd.
We are one of the most professional 2-wheeler painting line manufacturers and suppliers in China, also support customized service. Please feel free to buy advanced 2-wheeler painting line for sale here from our factory. Welcome to contact us for quotation.
Address: No. A802, Building 2, Tianan Digital Plaza, Longgang, Shenzhen, China
E-mail: victor@honglichang.com
WebSite: https://www.honglichang-paint.com/
