If you’ve ever sipped a cold bottle of water, breathed clean air, or even used a tube of sunscreen, you’ve likely benefitted from a distillation column—even if you didn’t know it. As someone who’s spent the last 12 years building, maintaining, and customizing these columns for chemical plants across North America, I’ve heard more than a few questions over the years: “Why is this old, tall metal tower so critical to our operation?” or “Can’t we just use another process that’s cheaper?” The short answer? Distillation isn’t just a chemical process—it’s the backbone of modern manufacturing, the quiet workhorse that turns raw, unrefined materials into the products we rely on every day. Today, I want to walk you through exactly how distillation columns work in the chemical industry, why they’re non-negotiable, and how we tailor our columns to fit the unique needs of every plant we partner with. Distillation Column

Let’s start with the basics, because it’s easy to write off a distillation column as a “big metal tube,” but that simplification misses the science that makes it powerful. At its core, distillation separates mixtures of liquids (or sometimes gases) that have different boiling points. Think of heating a pot of water on the stove with a drop of rubbing alcohol in it: alcohol boils at 173°F, way lower than water’s 212°F. If you cover the pot with a lid, the alcohol turns to vapor first, condenses on the cool lid, and drips into a separate cup. A distillation column is just a scaled-up, precision-engineered version of that same principle—only instead of a pot and a lid, it uses internal trays or packing material to create hundreds of tiny, repeated heating and cooling cycles inside the tower.
The column itself is a vertical steel vessel, usually anywhere from 20 feet to over 200 feet tall, depending on what it’s separating. At the bottom, a reboiler heats the raw mixture to its boiling point, sending vapor up through the column. At the top, a condenser cools the rising vapor, turning it back into liquid. That liquid flows back down the column, trickling over the internal trays or packing, while the vapor moves up. Where they meet—on each tray or every few inches of packing—vapor and liquid exchange heat, and the component with the lower boiling point moves into the vapor phase, while the higher boiling component stays in the liquid. By the time vapor reaches the top, it’s almost entirely made of the low-boiling point component, and liquid at the bottom is mostly the high-boiling point one. For chemical engineers, this is a way to get purities that other separation methods (like filtration or centrifugation) can’t touch—often 99.9% or higher.
Now, let’s get into the real-world applications, because this is where distillation columns earn their keep. I’ve worked with plants ranging from small specialty chemical makers to multinational oil refineries, and the use cases are as varied as the products they make. Let’s break down the biggest ones.
First up: petroleum refining, which is where distillation got its start more than 150 years ago. When crude oil comes out of the ground, it’s a mucky mix of hundreds of different hydrocarbons—from tiny methane molecules (that boil at -259°F) up to heavy asphalt (which boils at over 1,000°F). A refinery’s first step is a huge distillation column called an atmospheric crude tower. Crude oil is heated to 700°F and fed into the bottom of the tower. As the vapor rises, the tower is designed with temperature zones: at the top, the coolest end, we get gasoline and kerosene. Lower down, hotter zones produce diesel fuel, jet fuel, and heating oil. At the very bottom, the heavy residue goes to a vacuum distillation tower, which operates at reduced pressure to lower boiling points, separating out lubricants, waxes, and asphalt. I’ve seen columns like this that stand 150 feet tall—taller than a 15-story building—processing 200,000 barrels of crude a day. Without distillation, that crude is just black goo, not the fuels that power our cars, planes, and homes.
Next, specialty chemicals and pharmaceuticals—areas where purity is non-negotiable, and even tiny impurities can ruin a batch or make a medicine unsafe. Take, for example, a plant making ethanol for hand sanitizer or COVID-19 vaccines. Fermentation produces ethanol that’s only about 95% pure; the rest is water and trace impurities. To get 99.5% pure ethanol (the grade needed for sanitizer), you need a distillation column with special azeotropic or extractive distillation technology. Azeotropes are mixtures where the boiling points are identical, so regular distillation can’t separate them—we add a third component, like cyclohexane, to break the bond. In pharma, this is even more precise: when making paracetamol or ibuprofen, the active pharmaceutical ingredient (API) has to be 99.9% pure, with no leftover solvents or unreacted raw materials. Distillation columns designed for pharma use are made from stainless steel, have highly polished interiors to avoid contamination, and are often automated with real-time sensors to adjust flow and temperature minute by minute. Last year, we worked with a small biotech startup that was scaling up a new antibiotic; their old off-the-shelf column couldn’t hit the required purity, so we designed a custom packed column with a special packing material that reduced contamination and increased yield by 12%. That small gain meant they could get their product to patients faster, and that’s the kind of impact I don’t take for granted.
Another big application is the production of industrial gases—oxygen, nitrogen, argon, the gases used in food packaging, medical supplies, and metal cutting. Air is a mix of 78% nitrogen, 21% oxygen, and 1% argon, but to get pure nitrogen for keeping potato chips fresh or pure oxygen for hospitals, you have to separate these gases. This uses a cryogenic distillation column, which operates at super cold temperatures (below -300°F). Air is compressed, cooled, and fed into the bottom of the column. Since nitrogen boils at a lower temperature (-320°F) than oxygen (-297°F), it rises to the top as vapor, while oxygen is pulled out the bottom. Argon, which boils in between, is pulled out from a middle tray. We’ve built these columns for air separation plants that supply hospitals across the Midwest; when the pandemic hit in 2020, one of our clients increased their column capacity by 25% to meet the spike in oxygen demand, and that’s when I realized how vital these machines are beyond just factory floors.
Even the food and beverage industry relies on distillation columns, though many people don’t realize it. Craft distilleries that make whiskey or gin use small distillation columns, or “stills,” to separate alcohol from the fermented grain mash. The smoothness of a whiskey depends on how well the column separates ethanol from harsh, undesirable compounds like methanol or fusel alcohols. I’ve worked with a few craft distilleries that started out with basic pot stills but outgrew them as their brand grew; switching to a custom distillation column helped them make a more consistent product and scale production without sacrificing quality. Also, big beverage companies use distillation to make things like fruit juices, removing water to make concentrate, or to separate flavors for use in sodas and snacks.
Now, you might be wondering: why not use other separation methods, like membrane filtration or liquid-liquid extraction? For small-scale operations, those can work, but when you need to separate large volumes of materials with high purity and low cost, distillation is almost always better. Membranes can get clogged or degrade over time, especially with harsh chemicals at high temperatures, and liquid extraction uses solvents that have to be disposed of, adding cost and environmental risk. Distillation, when designed right, has a lower operating cost per unit of product, works with almost any liquid mixture, and can be adjusted to handle changes in feedstock or demand. That said, distillation isn’t perfect—it uses energy to heat and cool, which is why so many plants are working to optimize their columns to use less power, reduce emissions, and improve yield. That’s where our team comes in.
Over the years, we’ve learned that every plant’s needs are unique, so we don’t sell one-size-fits-all columns. Some clients need a column that runs 24/7 for 10 years straight with minimal maintenance; we build those with heavy-duty carbon steel and corrosion-resistant lining for harsh chemicals. Others work in industries where downtime costs $100,000 an hour, so we design columns with quick-access trays and remote monitoring sensors that alert us to small issues before they become big problems. For pharma and food clients, we use food-grade stainless steel and design columns that are easy to clean, meeting FDA and GMP standards. We also work with clients to retrofit existing columns to boost capacity or improve purity—last year, we retrofitted a refinery’s 120-foot atmospheric tower, replacing old trays with high-efficiency packing, which increased gasoline yield by 8% and cut energy use by 15%. That’s the kind of result that makes both our team and our clients happy.
If you’re a chemical plant manager, process engineer, or someone responsible for production, I know firsthand that choosing the right distillation column can make or break your operation. A poorly designed column can lead to low product purity, high energy bills, frequent downtime, and lost revenue. A well-designed, custom column can boost yield, reduce costs, help you meet regulatory standards, and even support your sustainability goals—whether that’s cutting emissions from energy use or reducing waste from lost product.
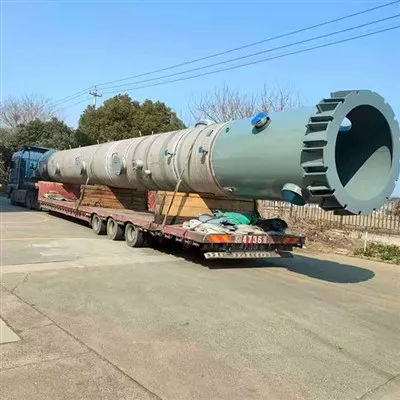
If you’re looking to upgrade an existing column, design a new separation process, or troubleshoot a persistent separation issue, I’d be happy to walk through your needs and discuss how our columns can work for you. We’ve worked with facilities of all sizes, from startups scaling their first API production to large refineries updating their entire distillation network, and we bring that 12 years of on-the-ground experience to every project.
Industrial Reactor References
- Seader, J. D., Henley, E. J., & Roper, D. K. (2020). Separation Processes Principles. Wiley.
- Petroleum Technology Gateway. (2022). Distillation in Crude Oil Refining. American Petroleum Institute.
- Food and Drug Administration. (2021). Current Good Manufacturing Practices (cGMP) for Pharmaceuticals. U.S. FDA.
- Cryogenic Society of America. (2019). Cryogenic Distillation for Air Separation. CSA Technical Bulletin.
Wuxi Quansheng Industrial Equipment Co., Ltd.
As one of the most professional distillation column manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Welcome to buy high quality distillation column for sale here from our factory. For price consultation, contact us.
Address: No.10, Fulaiqiao Road, Hudai Town, Binhu District, Wuxi City, Jiangsu Province, China
E-mail: 397293586@qq.com
WebSite: https://www.pmmatech.com/
